Three Parameters Lock Your Line Architecture
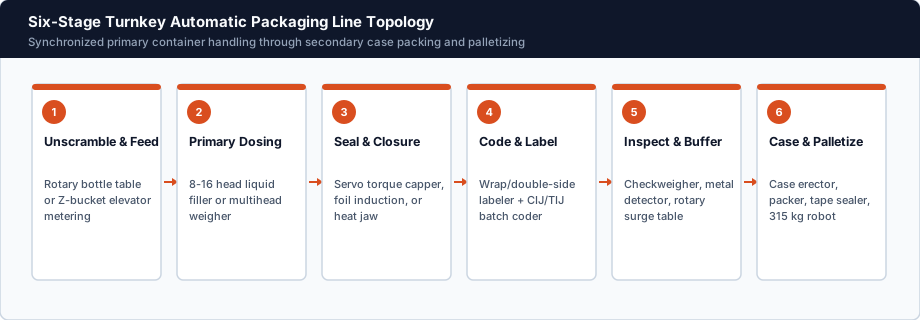
An automatic packaging line synchronizes container feeding, primary dosing, sealing or capping, date coding, weight/metal inspection, and secondary case packing under unified PLC speed control. Buying standalone machines piecemeal from separate catalogs routinely creates transfer dead-plates, mismatched conveyor heights, tip-overs, and conflicting handshake signals.
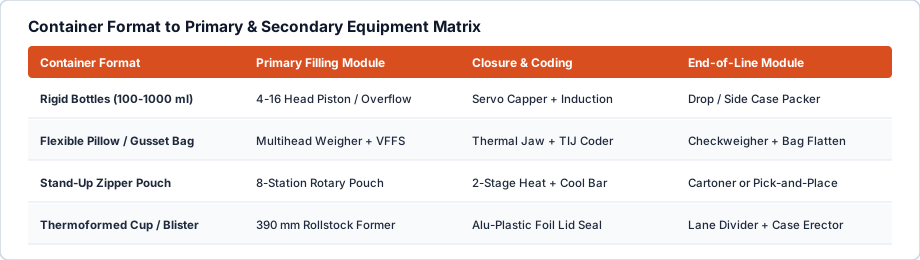
Before comparing individual machine models, lock three plant parameters: primary container geometry (rigid bottle/jar, vertical rollstock bag, or premade stand-up pouch), product flow behavior (free-flowing liquid, viscous paste, dusty powder, or fragile granule), and net shift output in bottles or bags per minute. Explore bottle packaging lines, bag and pouch packaging lines, and turnkey packaging line engineering for layout specifics.
Published Turnkey Line Envelopes by Format
Industrial turnkey installations cluster into four repeatable primary architectures depending on package rigidity and target output:
| Line Architecture | Container Scope | Published Speed Range | Core Utility Envelope | Typical End-of-Line |
|---|---|---|---|---|
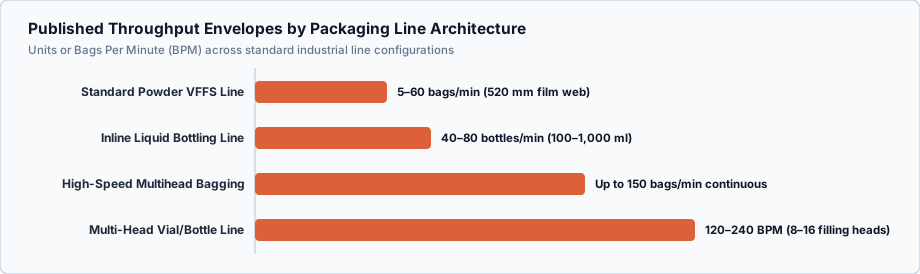
| Inline Liquid Bottling Line | 100–1,000 ml PET/HDPE/glass bottles (Ø 30–80 mm) | 40–80 BPM (2,500–4,800 BPH) | 220/380V, 0.8 MPa air, ~15–35 kW | Labeler + Drop/Side Case Packer |
| Multi-Head High-Speed Bottling | Vials, beverages, sauces (8–16 filling heads) | 120–240 BPM (6,000–12,000 BPH) | 380/440V 3-phase, 1.2 m³/min air | Rotary Buffer + Wrap Case + Robot |
| Multihead Weigher VFFS Line | Pillow & gusset bags (60–250 mm W, 520 mm web) | 10–70 BPM standard; up to 150 BPM | 220/380V, 4–9 kW, 0.65 MPa air | Checkweigher + Bag Flattener + Packer |
| Thermoform Rollstock Line | Rigid PS/PET blisters & cups (390 mm web, 1000–1400 μm) | 25–60 cycles/min multi-lane | 380V 3-phase, chilled water + air | Lane Merger + Cartoner / Case Erector |
For multi-machine layouts, also review packaging line configurations and automatic packaging line manufacturer delivery scopes.
Critical Line Integration Checks
- Transfer Plate & Conveyor Continuity: Standardize conveyor working height (typically 850 ± 50 mm) and side-rail adjusters so bottles and pouches cross machine boundaries without snagging.
- V-Curve Speed Headroom: Size capping, labeling, and case-packing stations 10–25% above nominal filler speed so rotary accumulation tables empty smoothly after a label splice.
- Single-Source Utility Drops: Consolidate 380V/440V three-phase power and dry 0.8 MPa air manifolds with local FRL filtration at high-cycle pneumatic cylinders.
Pre-RFQ Plant & Sample Verification
Measure clear ceiling height before specifying Z-bucket elevators + multihead weigher mezzanines (typically 3.6–4.5 m total stack height), and send filled/unfilled container samples to verify starwheel pockets and seal jaw widths.
Ready to size your floor layout? Submit container drawings and target BPM via our Project Brief.
Explore related specifications in Automatic Packaging Lines, Line Configurations & Specs, and submit your container throughput targets via Project Brief.