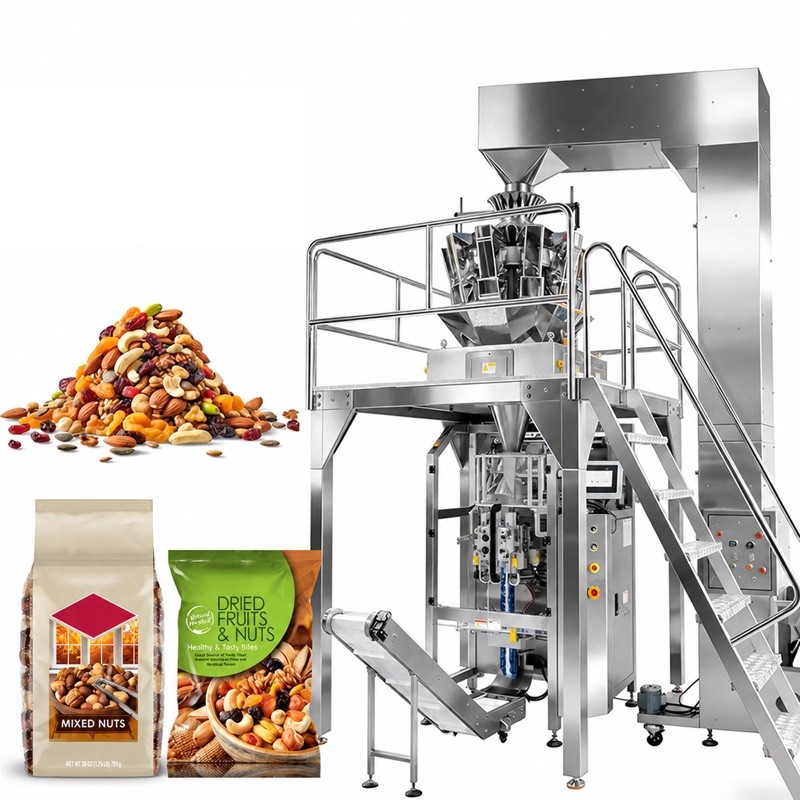
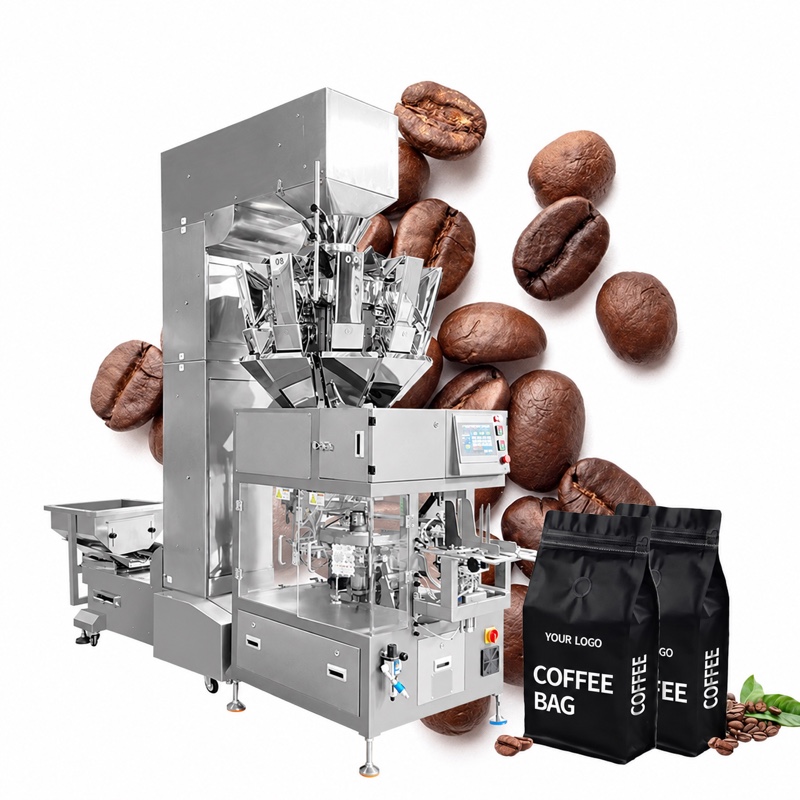
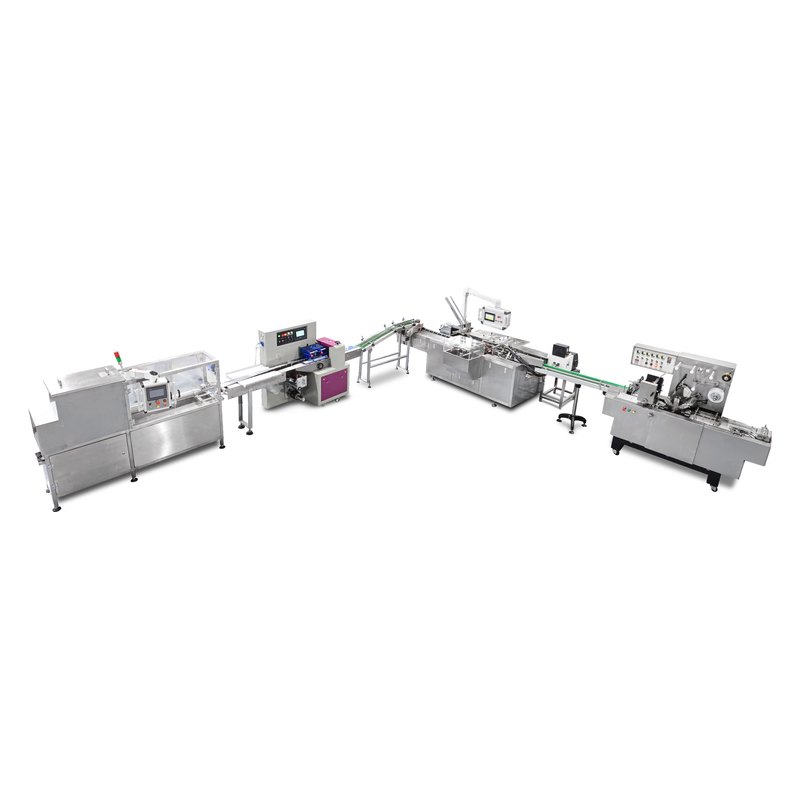
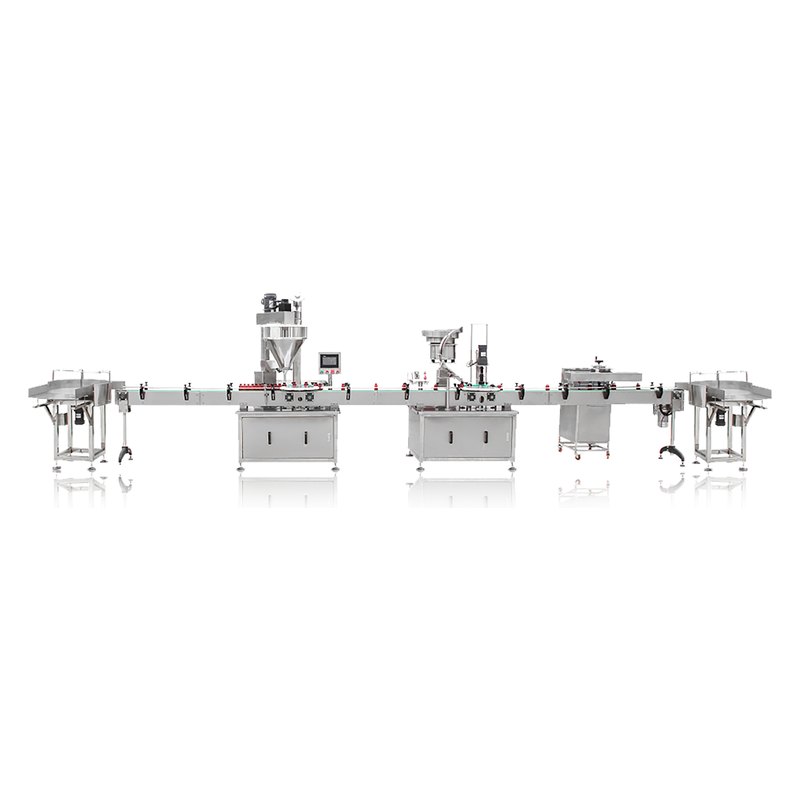
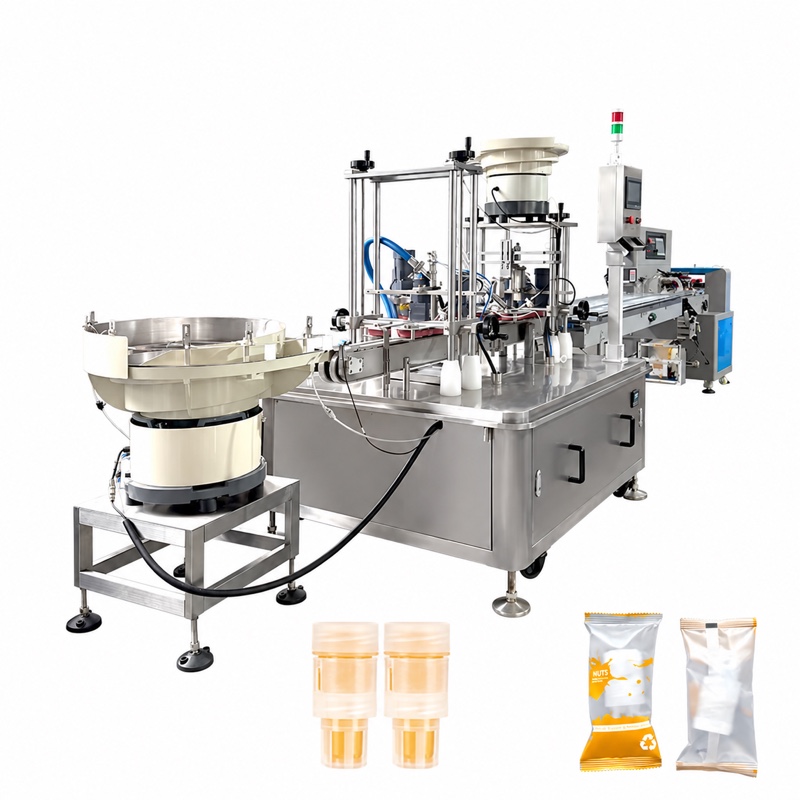
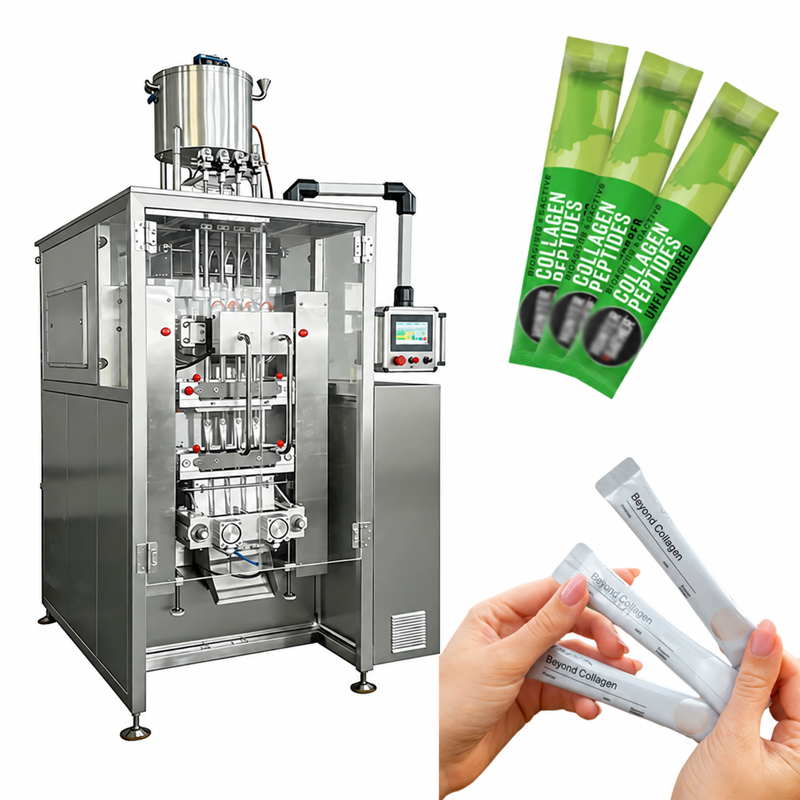
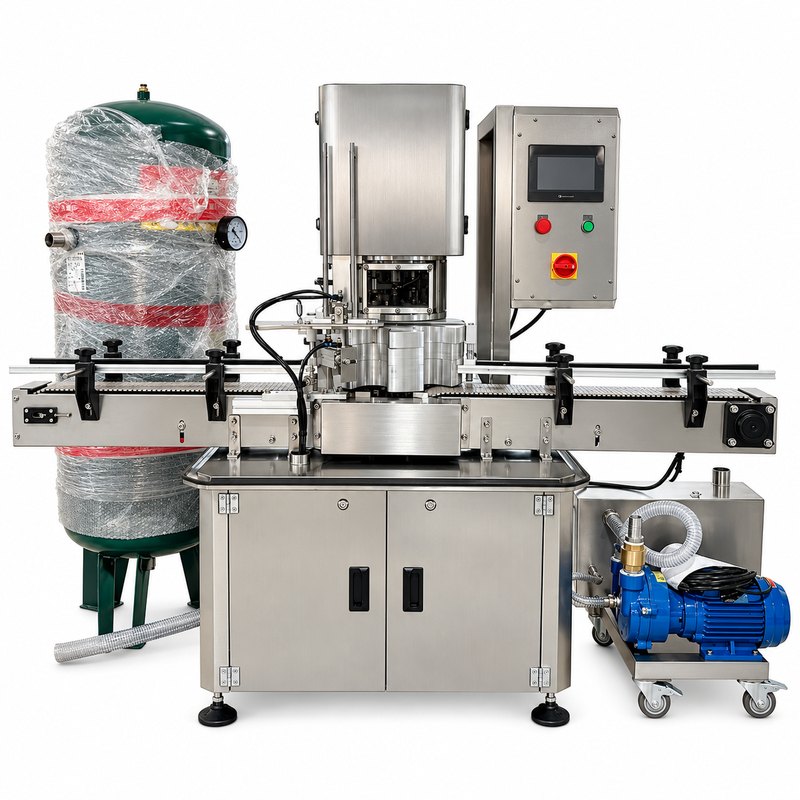
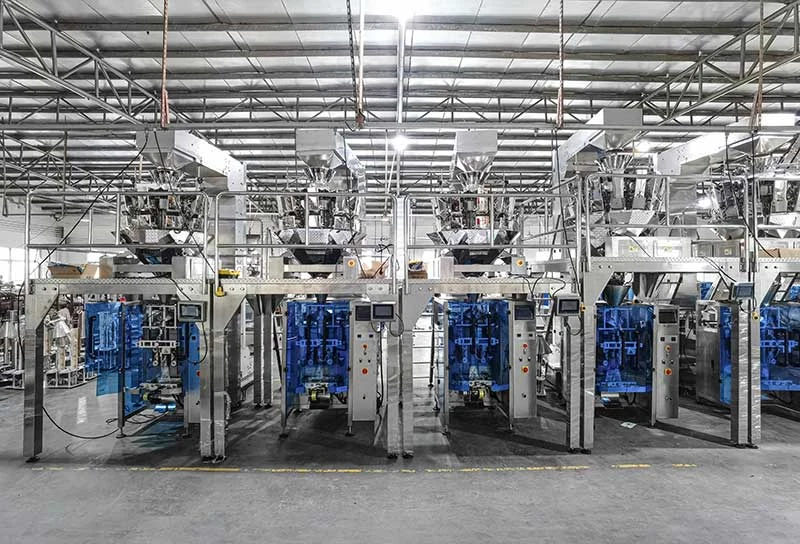
Prevent multi-vendor handoff gaps by defining upfront whether your project needs a standalone host machine, a synchronized dosing-to-sealing cell, or a full primary-to-overwrap turnkey line.
LEVEL 01SINGLE-FRAME HOST
Standalone Host Machine
Best for startups or batch rooms automating the core fill-and-seal bottleneck first while keeping infeed and case packing manual.
Included in LINEVO Scope
Primary VFFS bagger, LV-210 poucher, LV-400BF stick-pack, or LV-135ZFG seamer
Integrated Siemens PLC, Delta color HMI, and AirTAC pneumatic manifold
One verified format tooling set tested on your film or container in Foshan
Buyer / Plant Supplies
Manual hopper top-up or existing overhead surge bin
Manual off-pack table collection and master carton packing
Regulated ≥0.5 MPa clean dry air & plant electrical drop
Start with our two most requested multi-station turnkey spines on the top tier, or compare six dedicated pouch, stick-pack, rigid bottling, closure-dosing, and vacuum-seaming configurations below.
Downstream checkweighers, cartoners, and cellophane overwrappers are engineered with progressive 10–25% V-curve speed headroom so accumulation conveyors drain cleanly after film splices or carton magazine reloads.
Main programmable logic controller coordinating dosing, film/pouch indexing, and sealing interlocks.
CAB-ENC · 02
OMRONRotary Encoder, Control Relays & 24V Switching Power Supply
Phase-angle timing feedback, cabinet switching relays, and regulated 24V DC power supply.
CAB-DRV · 03
Delta ElectronicsHMI Color Touchscreen & Variable Frequency Drive (VFD)
Multi-recipe color operator terminal and inverter motor speed control for main drives and conveyors.
CAB-PNU · 04
AirTACPneumatic Cylinders, Solenoid Valves, Vacuum Gauge & FRL Unit
Actuation cylinders, pneumatic manifold valves, vacuum manometer, and air preparation unit.
Representative electrical, sensing, and pneumatic hardware fitted on LINEVO packaging configurations; exact part series or project-specified alternatives are itemized in your written quotation BOM.
04 · INTERACTIVE LINE CONFIGURATOR
Configure Your Packaging Line Engineering Brief
Select your primary container architecture on the left to review matched LINEVO station modules and pre-FAT specification parameters.
LINE-SPEC · 01Foshan FAT Ready
Liquid & Paste Bottling Line
Unscrambler, 4–16 head piston/overflow filler, capper, induction sealer, and labeler (40–200 BPM).
Every LINEVO line is CNC-machined, wired, and wet-tested under one roof in our 15,000+ m² Foshan facility—with two mandatory buyer verification gates highlighted before build freeze and before balance shipment.
STAGE 01
Pack & Room Intake
Review container dimensions, bulk density/viscosity, target shift output, and building column clearances.
STAGE 02BUYER GATE 1 · SAMPLE PROOF
Sample & Film Lab Test
Bench trial in Foshan on your physical product and laminate/closure to confirm dosing tolerance and seal integrity before build.
STAGE 03
2D CAD Floor Layout
Engineered DWG mapping straight or 90° L-turn conveyors, accumulation buffers, ceiling height, and utility drops.
STAGE 04
Itemized Scope Freeze
Written station list, format tooling table, voltage/frequency spec, and Siemens/OMRON/Delta/AirTAC cabinet BOM.
STAGE 05
CNC & SUS304 Fabrication
In-house machining, stainless contact finishing, and control-cabinet assembly inside our 15,000+ m² Foshan plant.
STAGE 06BUYER GATE 2 · PRE-SHIPMENT FAT
Pre-Balance Foshan FAT
Full-line synchronized run on your actual film reels, bottles, caps, and cartons—verified live or via multi-angle video before balance payment.
STAGE 07
Numbered Harness & Crating
Plug-coded inter-station signal cables, pre-saved bilingual HMI recipes, spare wear kit, and sea-worthy export cases.
STAGE 08
Startup & OEE Handover
Remote video walk-through or dispatched technician commissioning, operator changeover training, and preventive maintenance schedule.
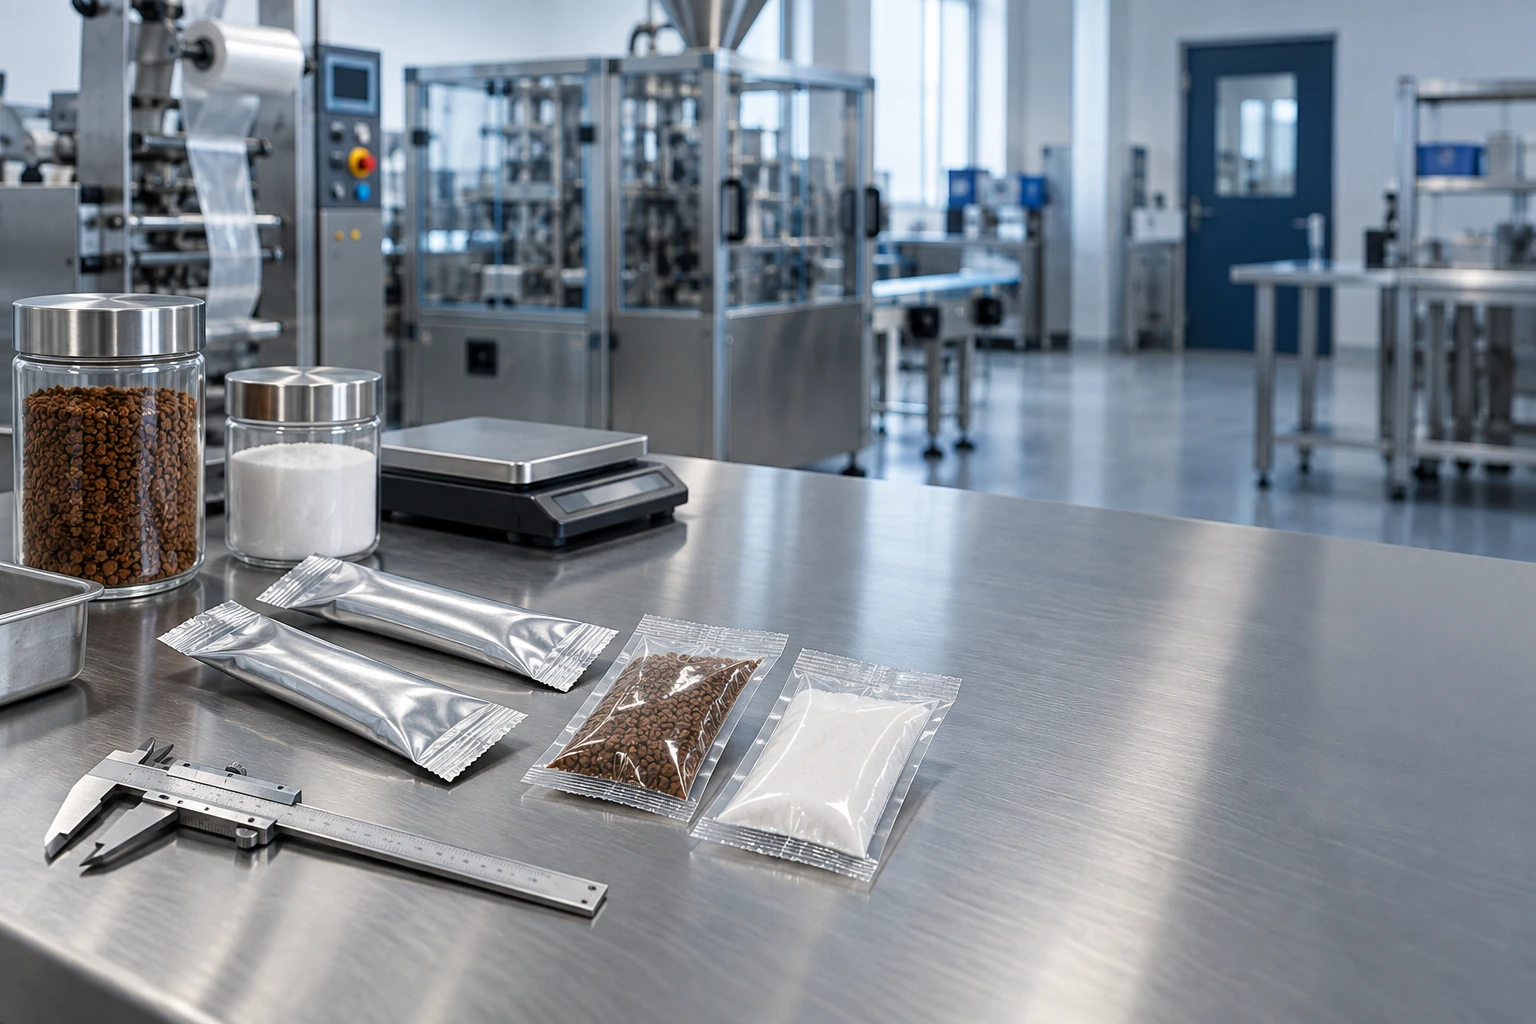
Foshan Turnkey Integration Bays — Parallel assembly and multi-station conveyor alignment across VFFS, rotary pouch, cartoning, and rigid bottling lines.Pre-FAT Sample & Laminate Lab — Gram-level checkweighing, caliper dimensional audits, and peel-strength verification on client-supplied packaging film.
06 · SYSTEM ARCHITECTURES & ENGINEERING HUBS
Core Line Configurations & Technical Specifications
Navigate technical reference sheets covering primary dosing, linear vs 90-degree room layouts, bottle indexing, flexible pouch automation, and OEE line sizing.
Size automatic packaging lines accurately: convert shift volume into nominal BPM at 78–82% OEE, balance multi-station speeds, and plan kW and air utilities.
Source directly from LINEVO in Foshan, Guangdong: 15,000+ m² workshop, 150+ staff, 50+ patents, 10 machine families, and 5,000+ global installations since 2013.
Line Sizing Calculators, Utility Charts & Buyer Guides
Run shift BPM and accumulation buffer equations, benchmark kW and compressed-air consumption, and review itemized turnkey line cost and FAT checklists.
Reference real LINEVO packaging machine dimensions (L × W × H mm), net weights (kg), electrical kW loads, voltages, and compressed air MPa requirements.
Understand what drives automatic packaging line cost across primary VFFS/LV-210/bottling modules, multihead weighers, T09 cartoners, tooling, and labor ROI.
Follow a 7-step engineering framework to choose the right automatic packaging line across LINEVO VFFS, LV-210 pouch, stick-pack, bottling, and cartoning.
Use LINEVO's Factory Acceptance Test (FAT) checklist to verify dosing accuracy, V-curve conveyor sync, seal integrity, and PLC fault interlocks before shipping.
Specify LINEVO powder jar and can seaming lines: bottle unscramblers, servo auger fillers, LV-135ZFG automatic vacuum can seamers (25–35 CPM), and labelers.
Direct engineering answers on LINEVO turnkey line integration, room clearances, electrical standards, and pre-shipment Factory Acceptance Testing in Foshan.
Need a Line Speed & Floor Fit Check?
Send container dimensions and shift output goals directly to our Foshan systems engineering team.
What project details are needed to engineer a straight-line or corner packaging layout?
Share your room length, width, clear ceiling height under overhead beams, container or bag dimensions, target fill weight, shift throughput goal, and local electrical supply (220 V single-phase or 380 V/480 V 3-phase, 50/60 Hz).
How are multi-station line speeds and sealing tolerances verified before shipment?
Every turnkey line undergoes Factory Acceptance Testing in our 15,000+ m² Foshan workshop using your actual film reels, bottles, caps, and folding cartons to verify dosing accuracy, V-curve conveyor transfers, and seal integrity.
How should downstream cartoners and 3D overwrappers be speed-matched to primary fillers?
Downstream checkweighers, T09 cartoners, and LV-BT280 / LV-BT350 3D cellophane overwrappers (30–80 boxes/min) are engineered with 12–25% V-curve speed headroom above the primary filler so accumulation conveyors clear smoothly after film or carton magazine reloads.