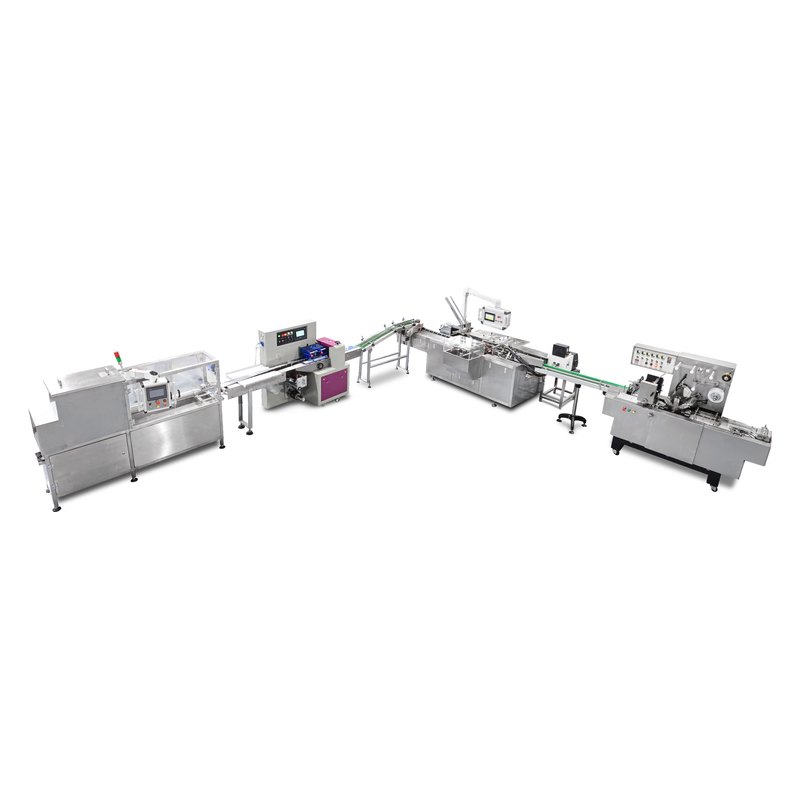
What It Is Built For vs. When to Choose Another Configuration
Use this rapid application screen to confirm whether 90° Corner Cartoning & Overwrap Line matches your container geometry, product flow behavior, and target throughput before freezing specifications.
Use It For
- Existing production rooms with limited bay length that still require automated pouching, cartoning, weight sorting, and 3D cellophane wrapping.
- Clean-zone separation layouts where primary wet/paste pouching sits in one room leg and dry carton/cellophane finishing turns 90° toward shipping.
- Single-operator U-cell or L-cell staffing where raw pouch film and carton/cellophane magazines sit within a few steps of the inner corner.
- Dense pastes, shisha blends, and portioned inner packs confirmed via Foshan sample testing.
When to Choose Another Configuration
- Your building has an open linear bay where an end-to-end straight conveyor spine avoids a 90-degree turning unit.
→ Switch to Straight-Line Pouch, Cartoning & Cellophane Line - Your primary pack is a rigid jar or bottle requiring unscrambling, auger/piston dosing, screw capping, and wrap labeling.
→ Switch to Automatic Bottle Filling, Capping & Labeling Line - You are packing dry granules into standalone rollstock pillow bags without outer cartons.
→ Switch to Multihead Weigher VFFS Bagging Line
Technical Specifications & Operating Conditions
This multi-station or format-specific LINEVO configuration (hookah-corner-line) is dimensioned directly from your physical product sample, container/carton drawings, and production room layout.
| Configuration Parameter | LINEVO Architecture | Project Verification Condition |
|---|---|---|
| LINEVO Equipment Family | T05 Corner-Type 5-Station Packaging Line | Left-hand or right-hand 90° layout engineered to room DWG. |
| Station Sequence | Horizontal Packer → Inclined/Turning Transfer → Cartoner → Weight Sorter → Cellophane Wrapper | Station order and buffer length tailored per room. |
| Space Advantage | Shortens required bay length vs. linear spine | Send room L × W × H and doorway dimensions for layout fit. |
| Application Validation | Sample run on client paste/pouch + folding carton | Verifies 90° box/pouch orientation stability prior to shipment. |
What Is Included vs. What We Review Per Project
Clear scope boundaries prevent startup surprises between the base machine and project-specific dosing, tooling, and plant interfaces:
Included in Core Machine Scope
- Horizontal high-speed primary pouch packing machine
- Weighing / weight-sorting scale module
- Automatic cartoning machine loading pouches into boxes and folding flaps
- Small-box transparent cellophane wrapping machine
Reviewed & Specified With Your Quotation
- 90-degree turning conveyor angle (left-hand vs. right-hand turn) and incline transfer matched to your exact room CAD drawing
- Wall clearances, column offsets, and operator access aisles around all five stations
- Site voltage/frequency panel build, batch coding, and sample trial verification
Working Sequence & Shop-Floor Countermeasures
Step-by-Step Operating Cycle
- STEP 01Primary pouches are formed, filled, and sealed continuously on the horizontal packing machine along the first leg of the line.
- STEP 02An inclined and 90-degree turning conveyor re-orients packs cleanly around the room corner without skewing seal edges.
- STEP 03Pouches enter the cartoning machine, which erects folding boxes, inserts each pouch, and closes carton flaps.
- STEP 04Filled cartons pass across the weight-sorting scale to reject off-weight boxes before the final station applies a tight transparent cellophane overwrap.
Real Production Floor Failure Modes & LINEVO Countermeasures
Countermeasure: Engineered turning conveyor rails and positive transfer guides maintain consistent pack orientation entering the cartoner and cellophane wrapper.
Countermeasure: Custom station spacing and left-or-right 90° corner geometry mapped directly onto your plant's architectural DWG before fabrication.
Countermeasure: Downstream weight-sorting station between cartoning and cellophane wrapping Diverts under- or overweight boxes automatically.
Countermeasure: Folding the five stations around an L-corner clusters HMI panels, carton magazines, and BOPP film reels around one central operator zone.
Comparing Quotations? Check These 5 Things First
5-Point Buyer Quotation Audit
- Speed Test Conditions vs. Shift OEE: Confirm whether quoted bags/boxes per minute reflect dry-cycle empty-film speed or filled product at your exact target weight, and plan net shift output using a realistic 0.70–0.85 OEE factor.
- Dosing & Upstream/Downstream Handshake: Verify mechanical chute/conveyor transitions and PLC ready/interlock signals between scales, primary sealers, cartoners, and checkweighers.
- Utility Power & Clean Dry Air Split: Match electrical panel build to your exact factory voltage, phase, and frequency (e.g., 220 V single-phase vs. 380 V/480 V 3-phase, 50/60 Hz) and confirm regulated oil-free dry air MPa and m³/min.
- Format Tooling for Extra Pack Sizes: Identify which pack dimensions adjust via HMI/handwheels versus which require dedicated forming collars, rotary discs, sealing chucks, or carton molds.
- Pre-Shipment Sample & Film FAT Run: Ensure the contract specifies a Foshan Factory Acceptance Test running your physical product samples and printed laminate reels or cartons before balance shipment.
Pre-Dispatch Foshan FAT & Project Sequence
Bench check of your product flow, piece geometry, and film/carton tolerances in Foshan.
Signed station list, utility schedule, format tooling table, and 2D CAD floor layout.
In-house CNC machining, SUS304/316L fabrication, and PLC electrical assembly.
Live or multi-angle video acceptance run on your actual packaging material before crating.
Sea-worthy export cases, bilingual HMI recipes, spare wear kit, and remote/on-site commissioning.
Control Cabinet & Pneumatic Hardware BOM
Main programmable logic controller coordinating dosing, film/pouch indexing, and sealing interlocks.
Phase-angle timing feedback, cabinet switching relays, and regulated 24V DC power supply.
Multi-recipe color operator terminal and inverter motor speed control for main drives and conveyors.
Actuation cylinders, pneumatic manifold valves, vacuum manometer, and air preparation unit.
Representative electrical, sensing, and pneumatic hardware fitted on LINEVO packaging configurations; exact part series or project-specified alternatives are itemized in your written quotation BOM.
Frequently Asked Questions
Can the 90-degree corner turn be built as either a left-hand or right-hand L-layout?
Yes. During layout engineering, LINEVO configures the turning conveyor and operator-side doors/HMIs for either a left-hand or right-hand 90-degree turn to match your room doors, columns, and material flow.
Why is weight sorting placed after cartoning in the corner-line sequence?
Weighing the closed carton immediately before cellophane wrapping confirms both full primary pouch fill weight and proper carton/leaflet presence before sealing the box inside tamper-evident BOPP film.
What room details should we send to get a 2D corner-line CAD drawing?
Provide room length and width, column coordinates, ceiling height, raw material entry and finished pallet exit doors, plus pouch and carton dimensions.